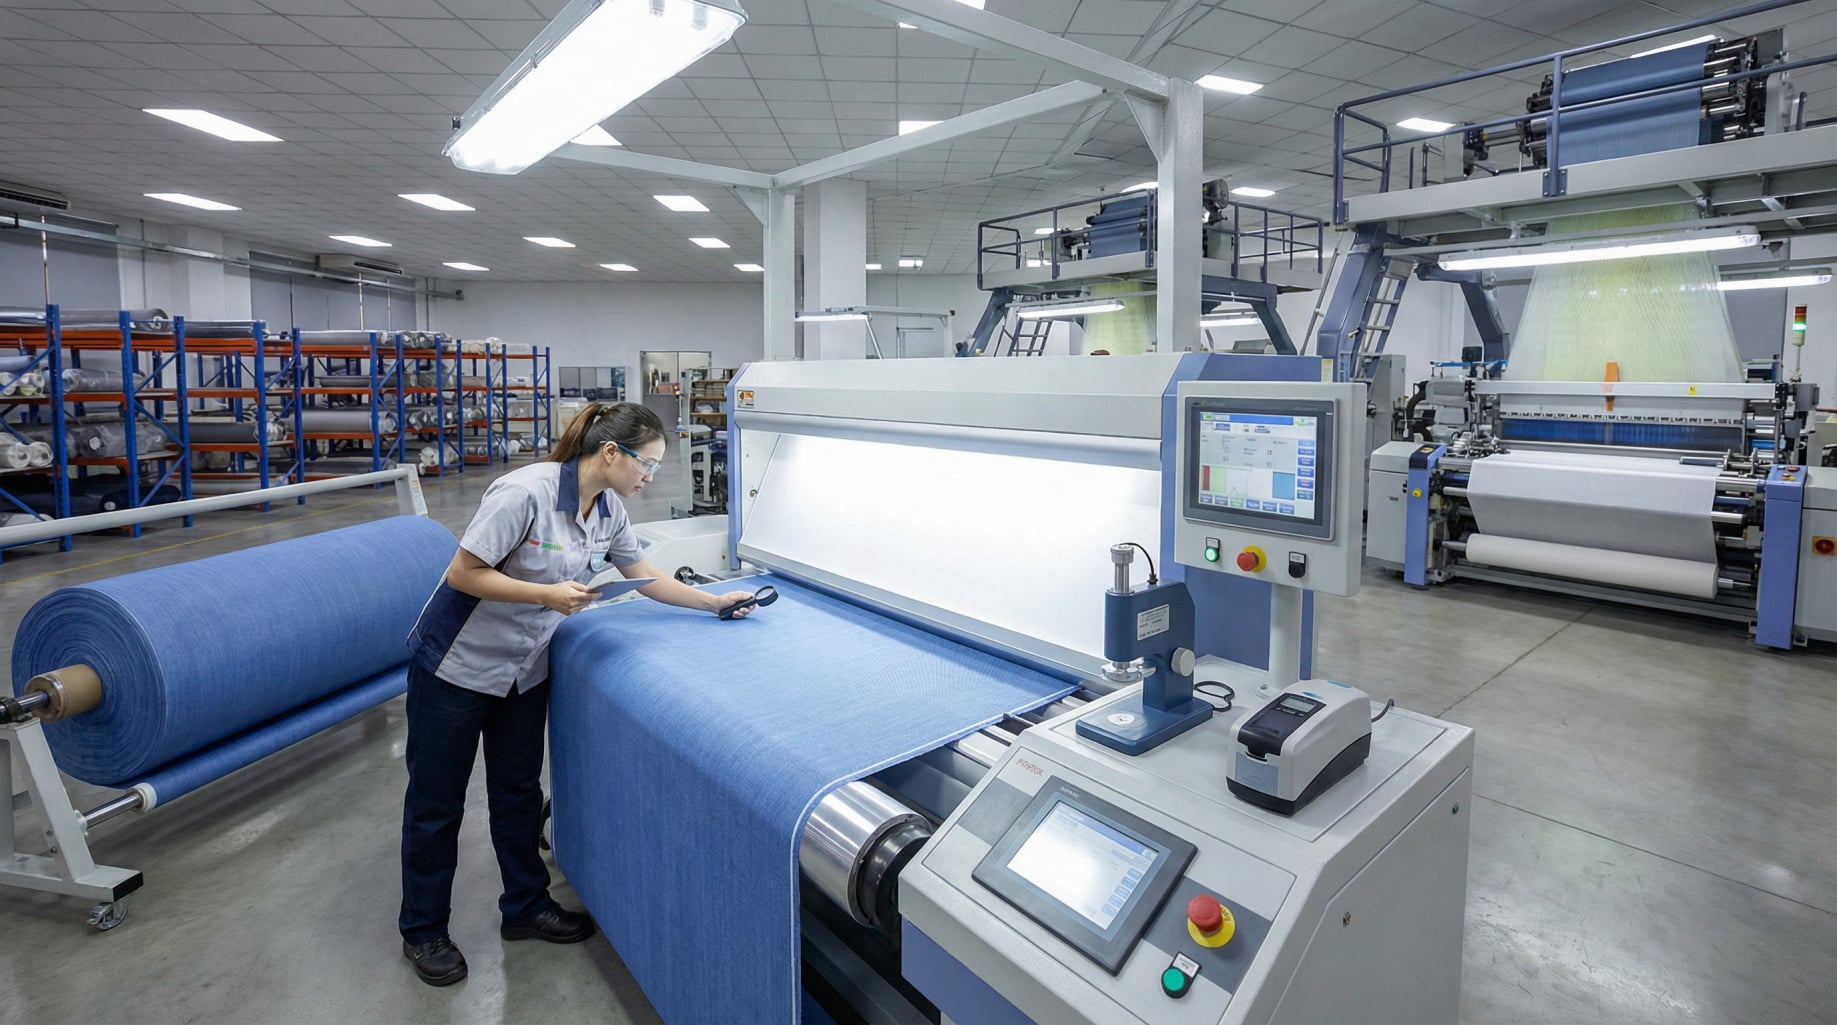
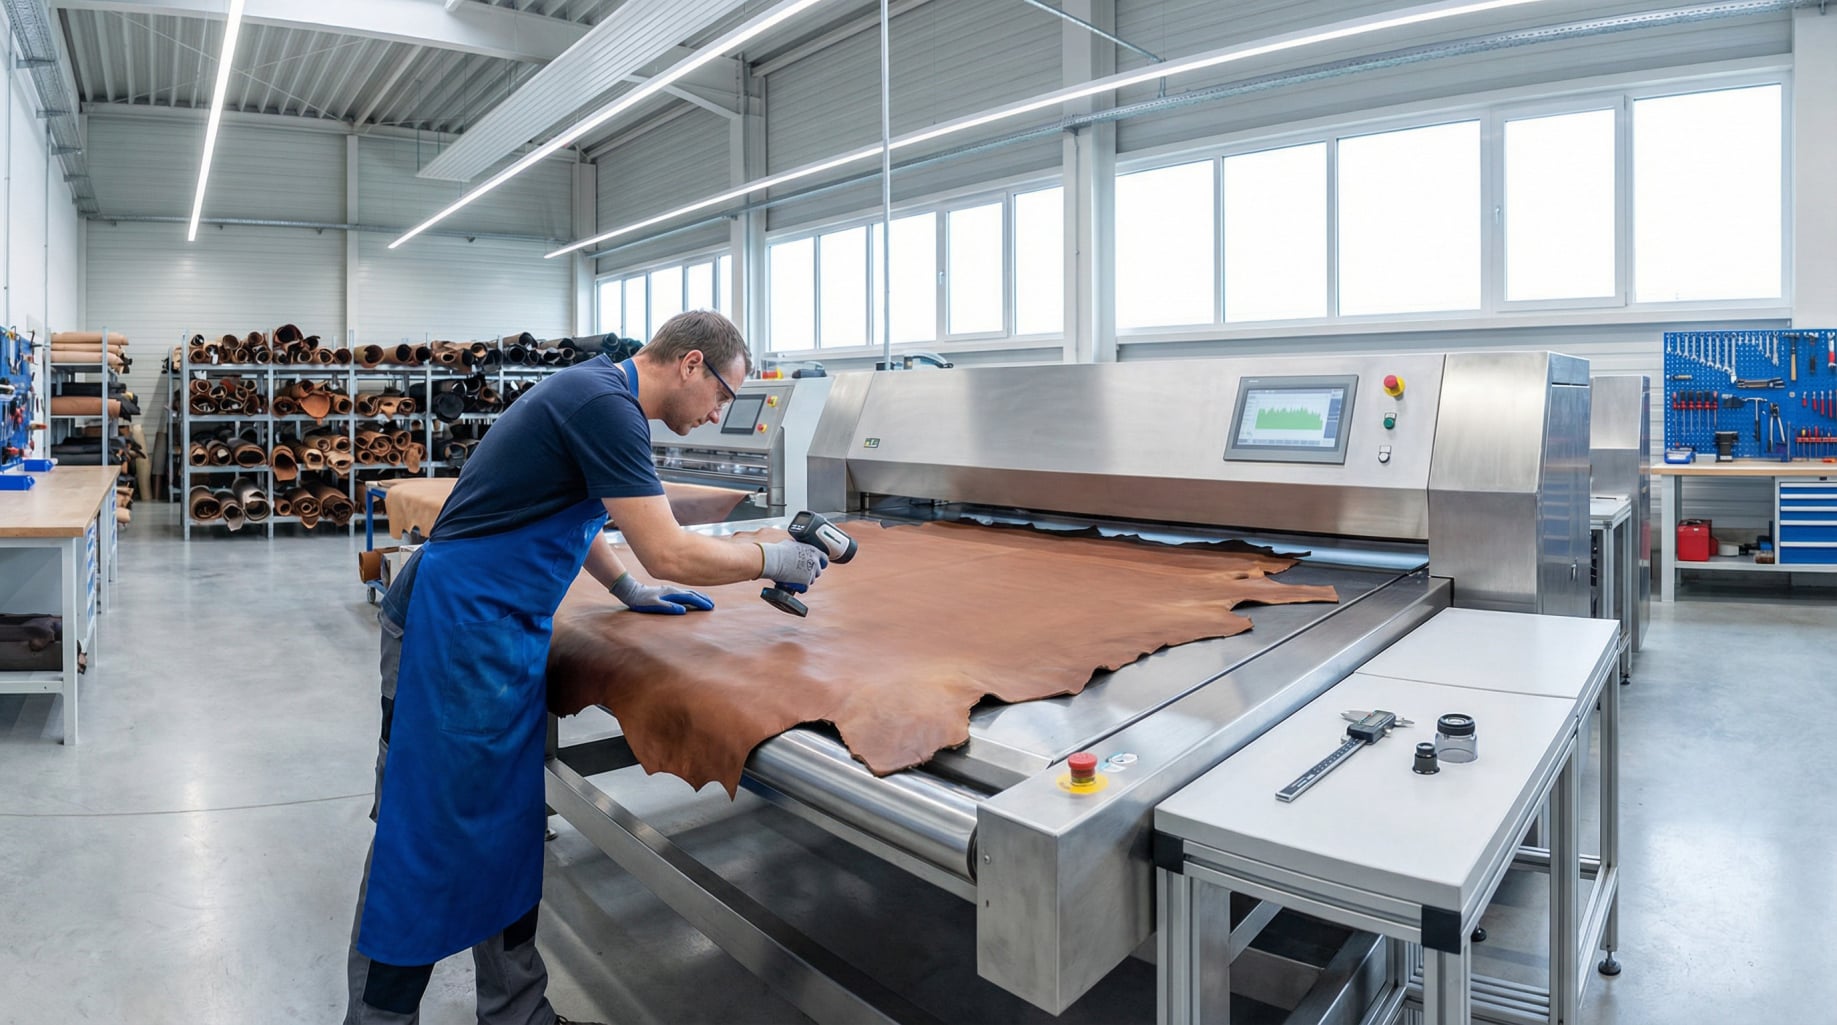
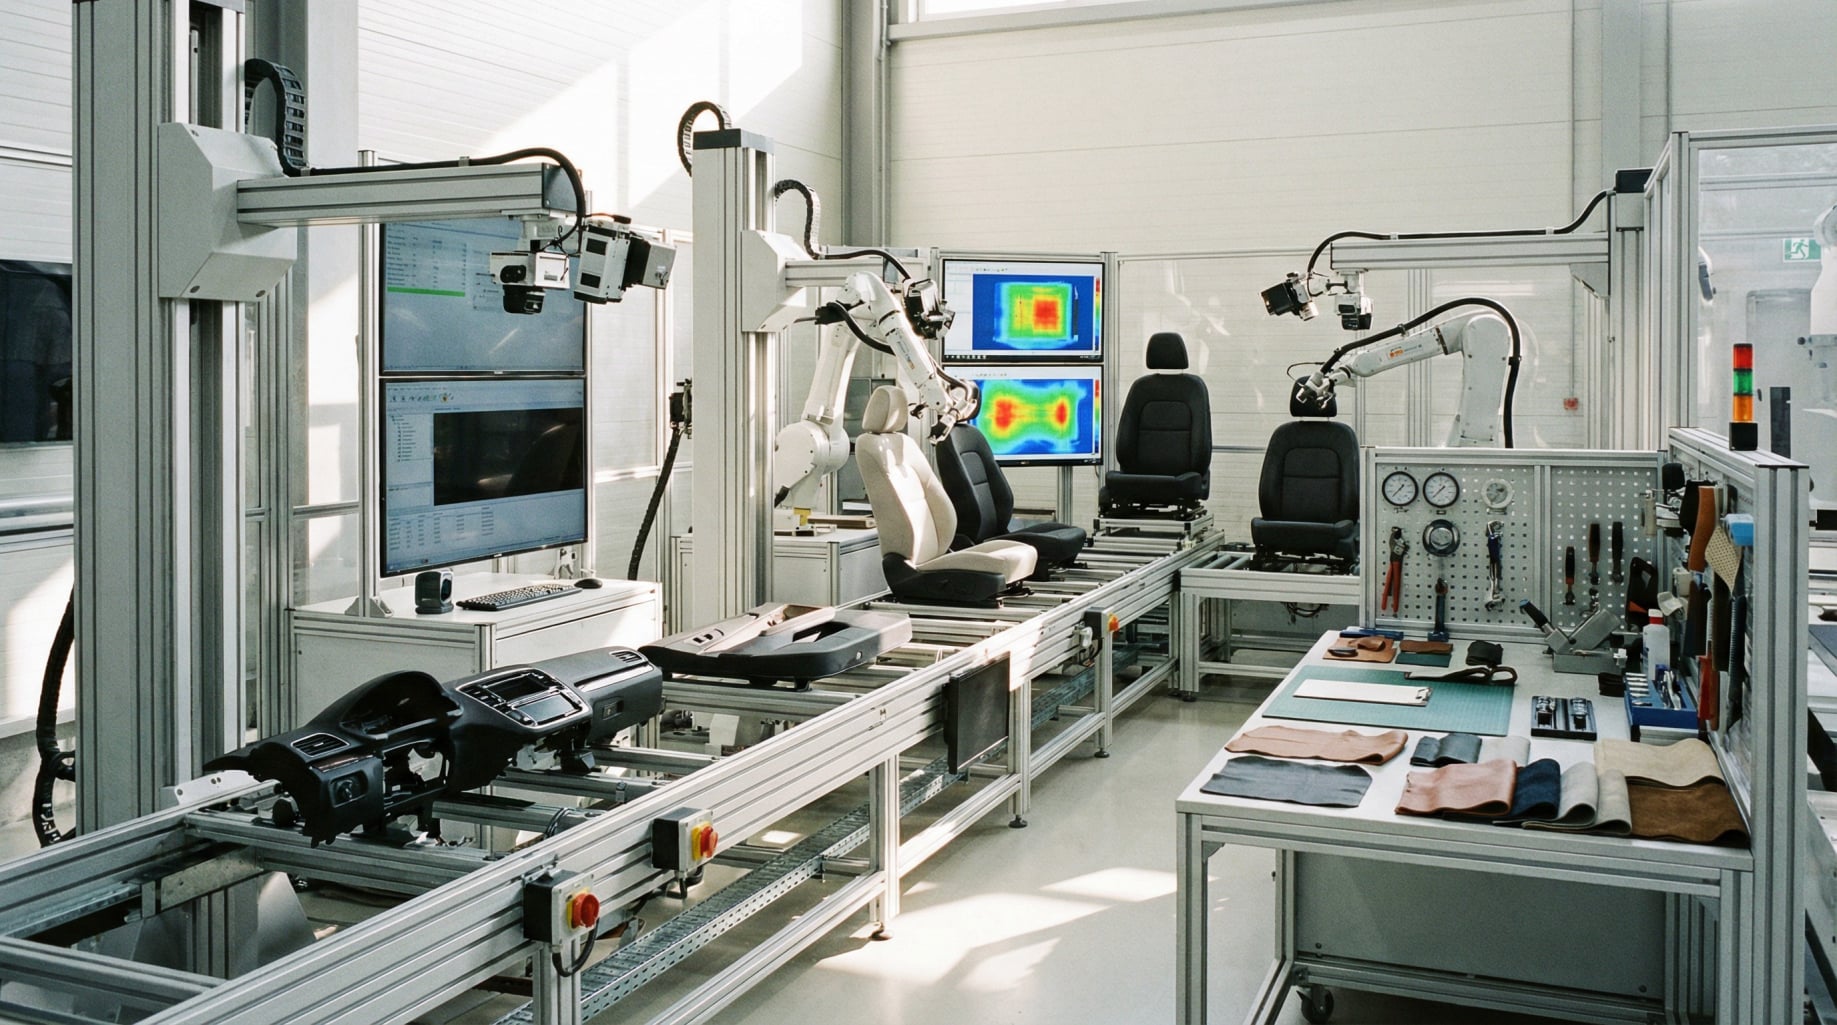
Computer vision is the ability of computing systems to interpret and understand the visual world exactly as the human eye does, but with the speed, precision and consistency that only a machine can guarantee.
Through cameras, sensors and artificial intelligence algorithms, vision systems analyse images and data in real time to detect defects, classify objects, measure dimensions and make decisions without interruptions, without fatigue errors, without subjective variability.
In industrial environments, computer vision transforms inspection from a manual, discontinuous process into continuous, traceable and scalable quality control
Industrial Quality Control & Sorting
Food & Beverage Processing
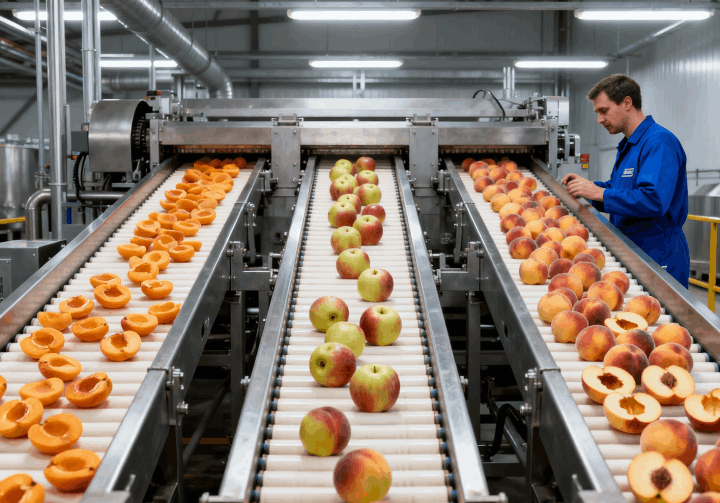
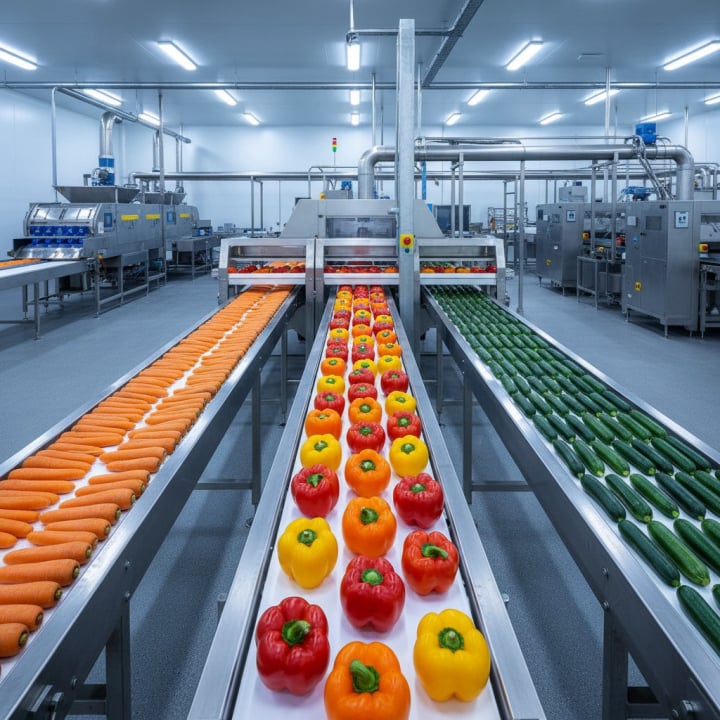
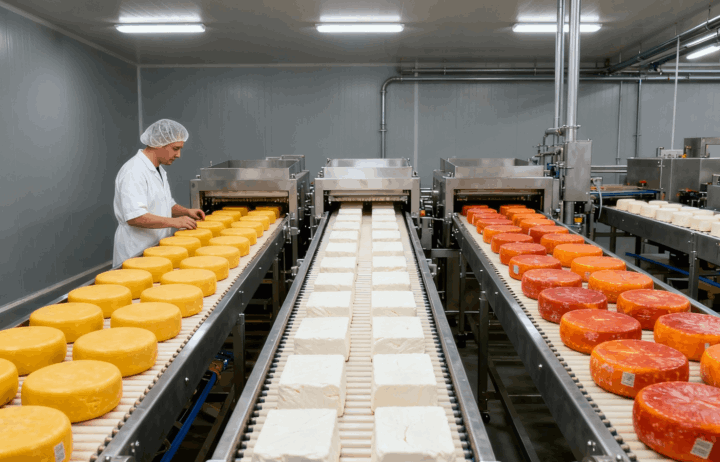
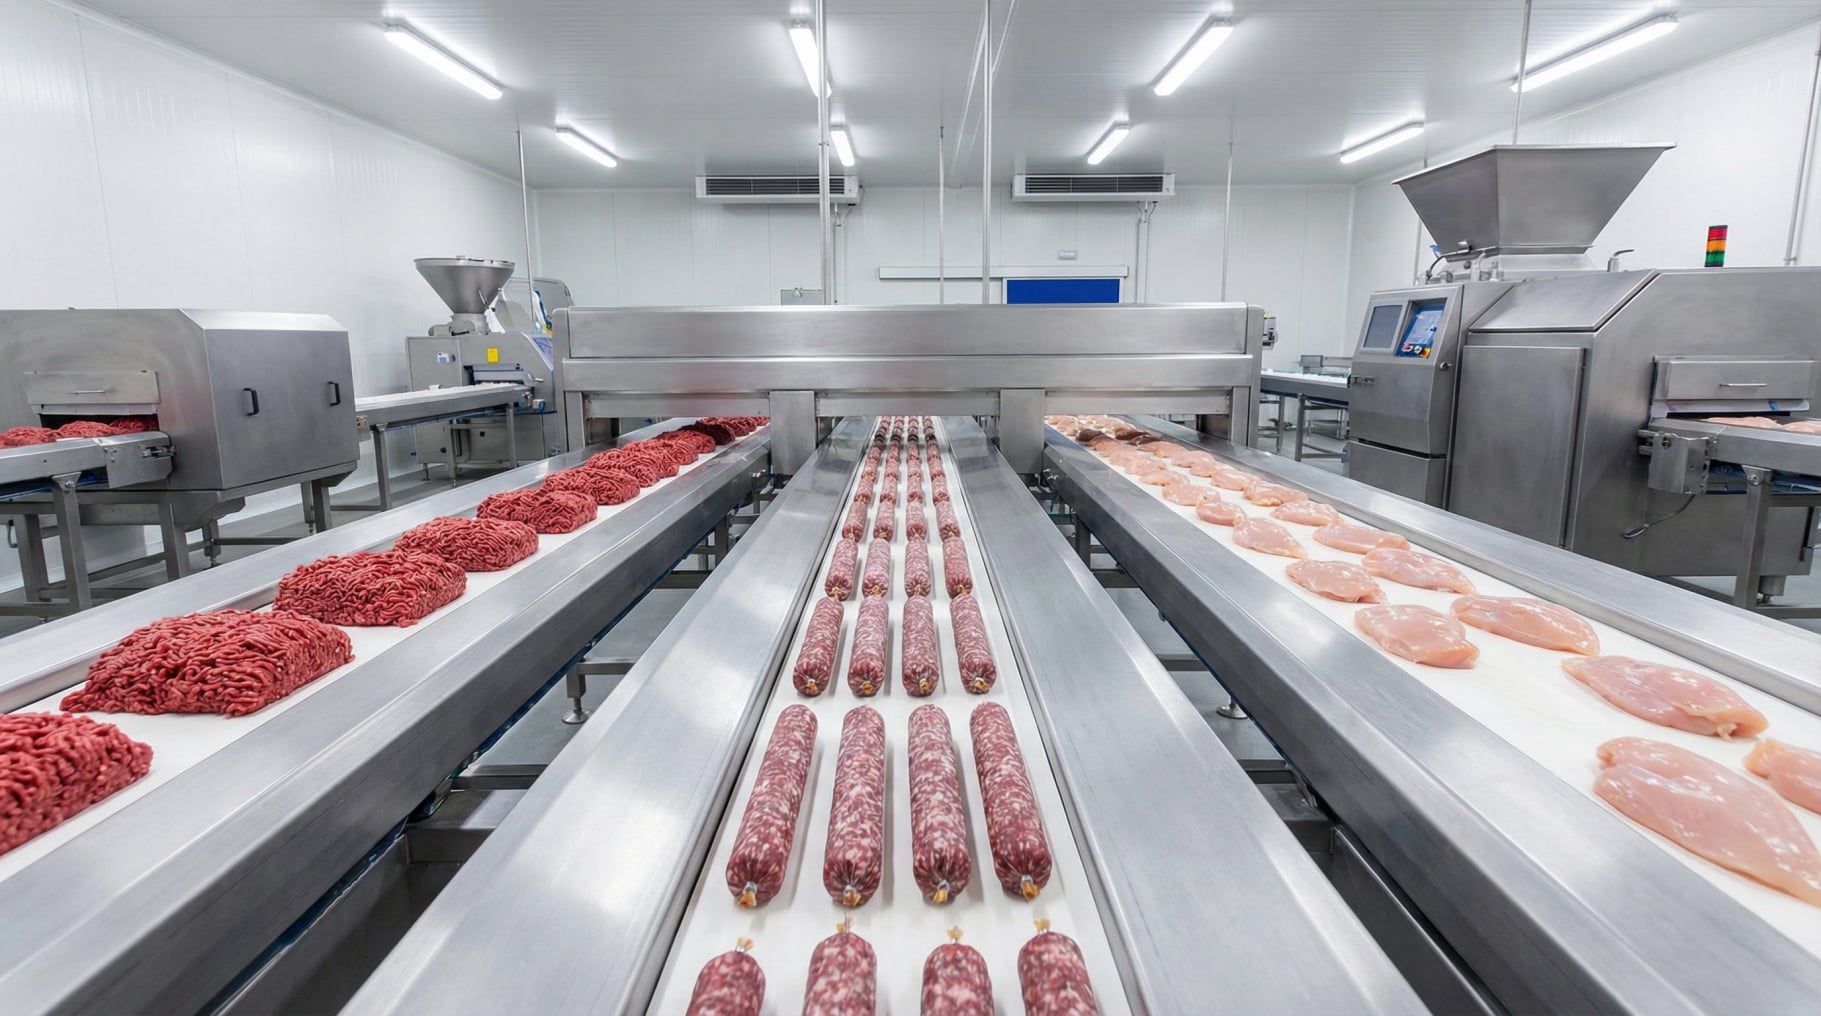
Consumer & Industrial Manufacturing
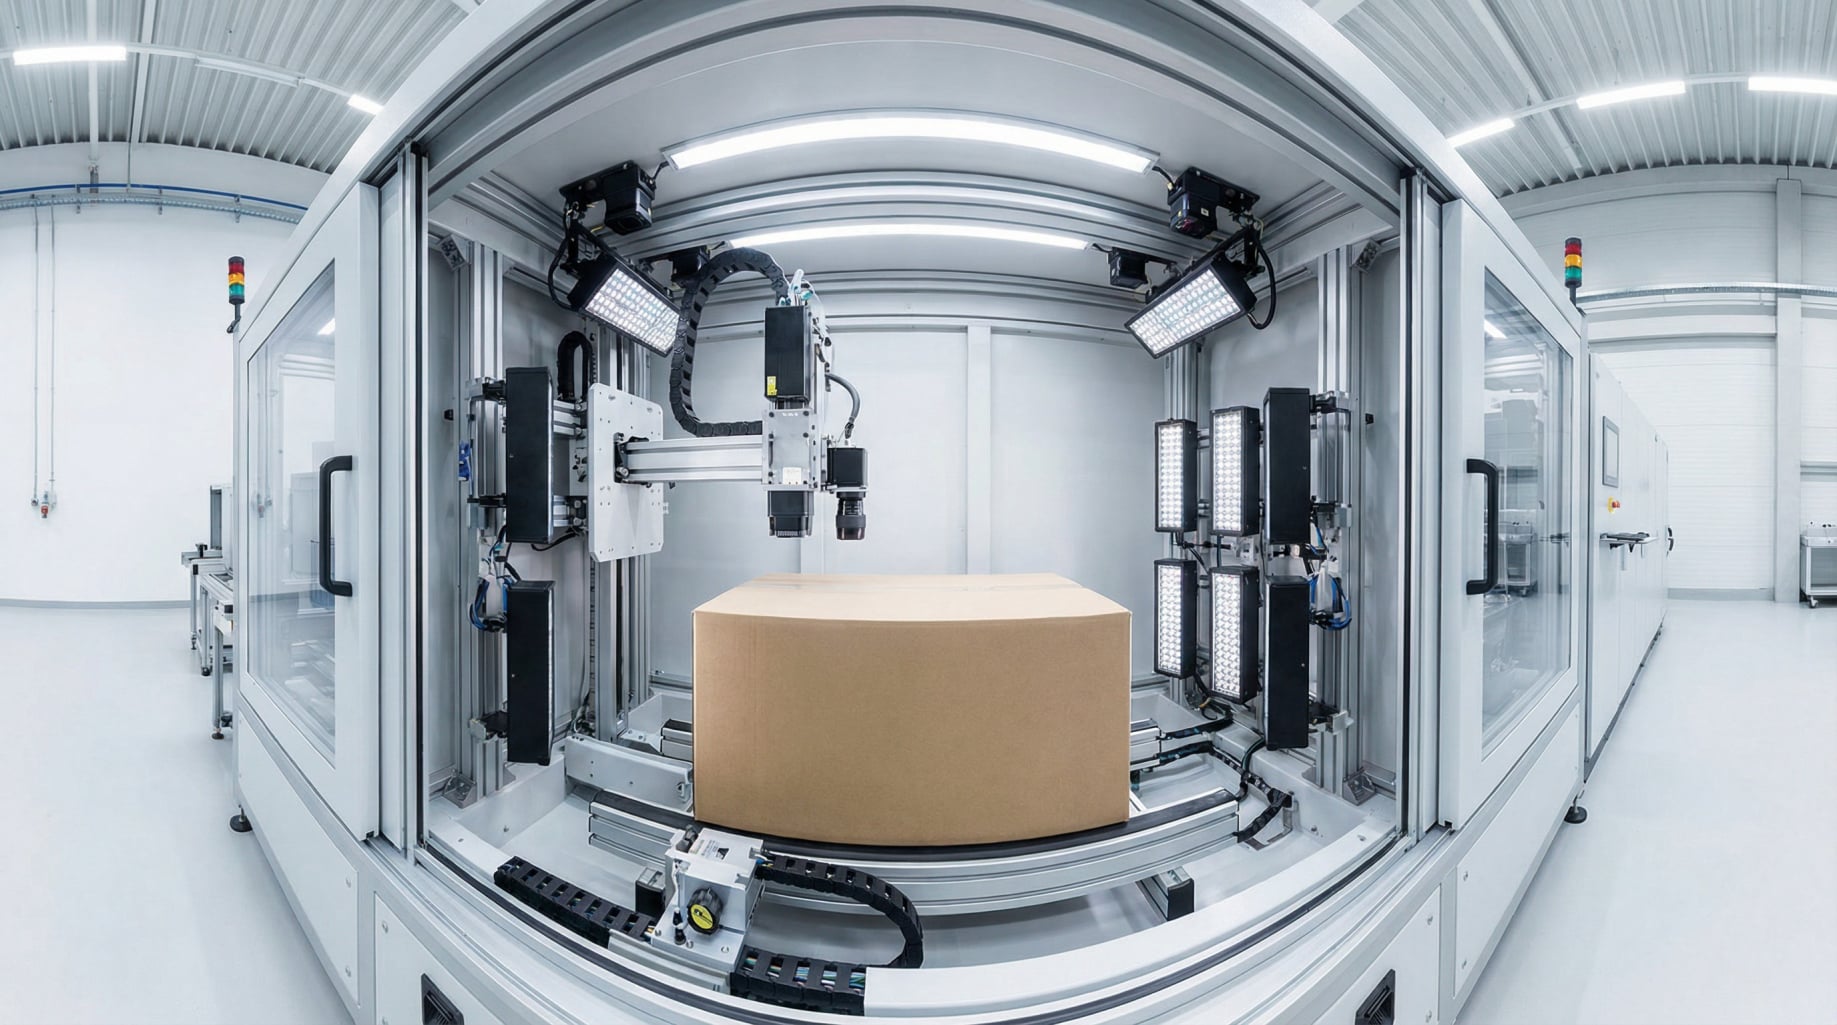
Multisensing
360° Vision
Fully Adaptable
100% Automated
30% Efficiency Improved
70% Waste Reduced
Benefits for you
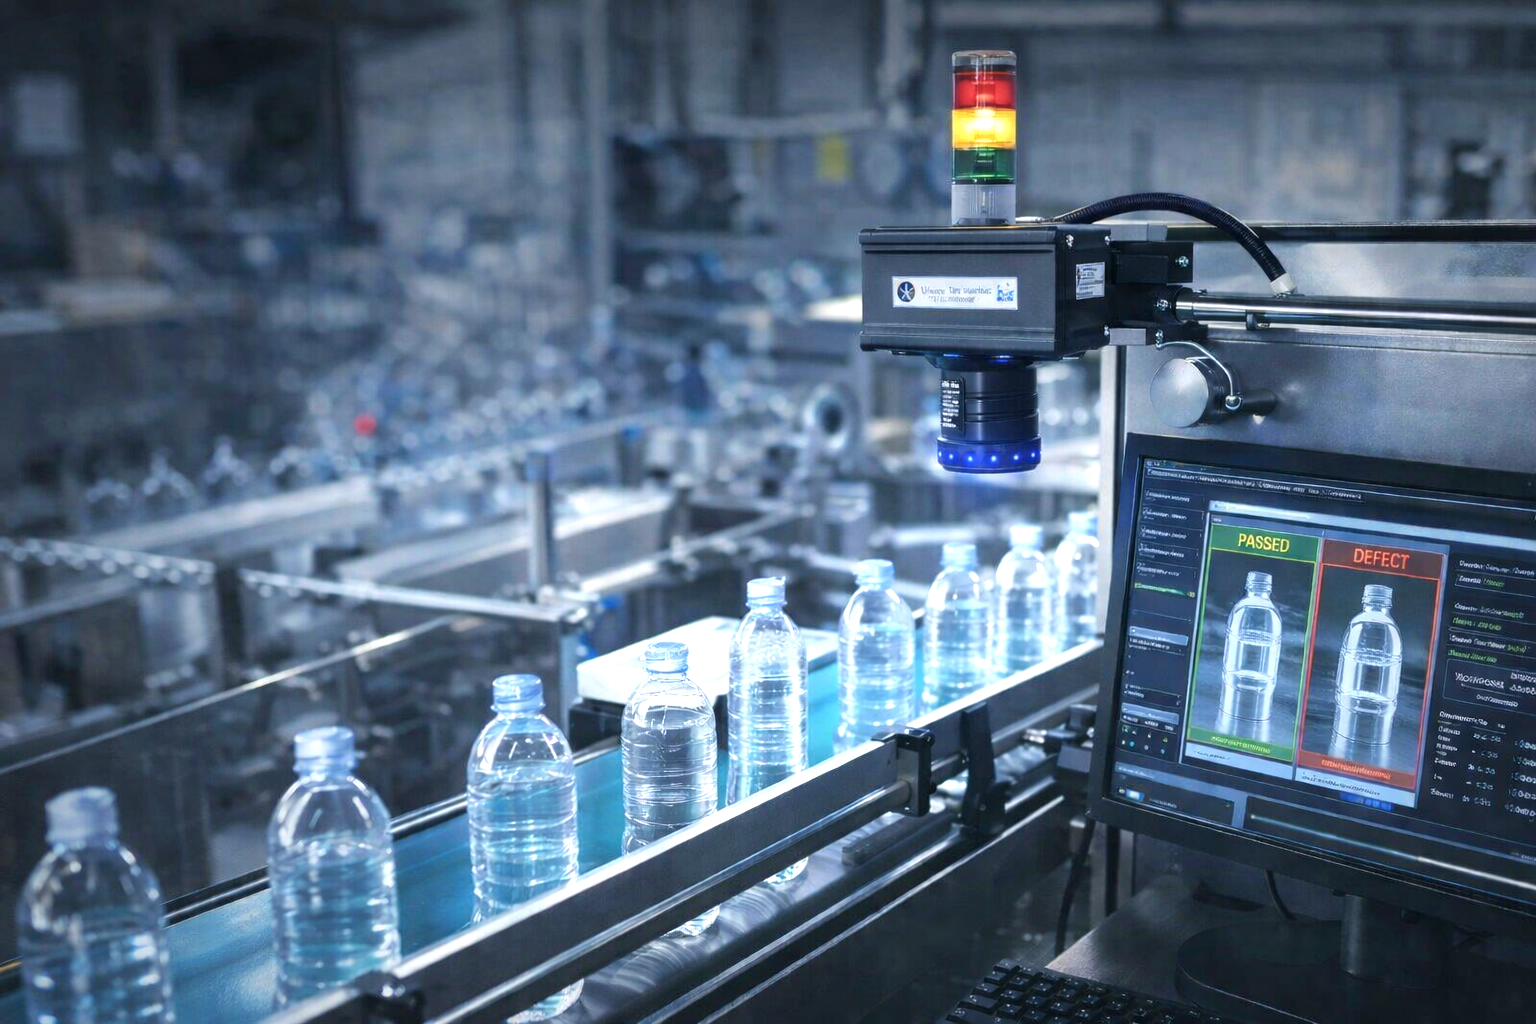
Automated Quality Assurance
Streamline your production with real-time, automated inspection systems that guarantee product compliance and reduce reliance on manual checks. Capture and document quality data for every item with precision, ensuring consistent standards across your entire output.
Read More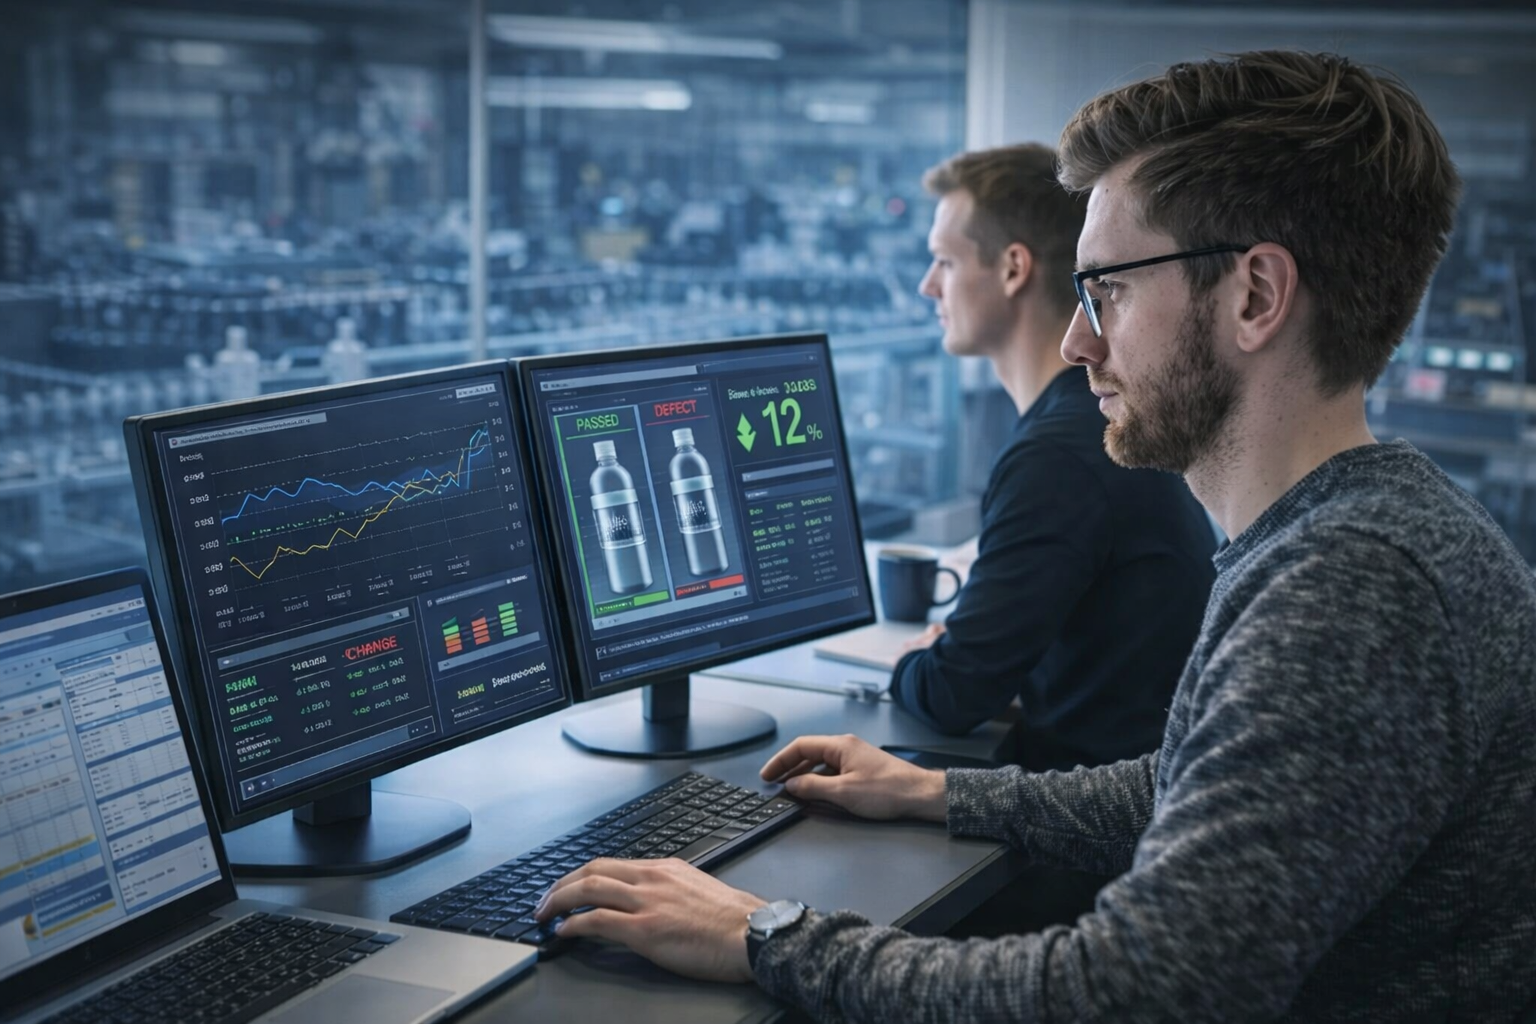
Leverage Quality Insights
By automating and digitalizing inspections, manufacturers unlock valuable data on production trends and performance. Actionable analytics and process feedback enable continuous optimization, helping to fine-tune operations and drive higher efficiency.
Read More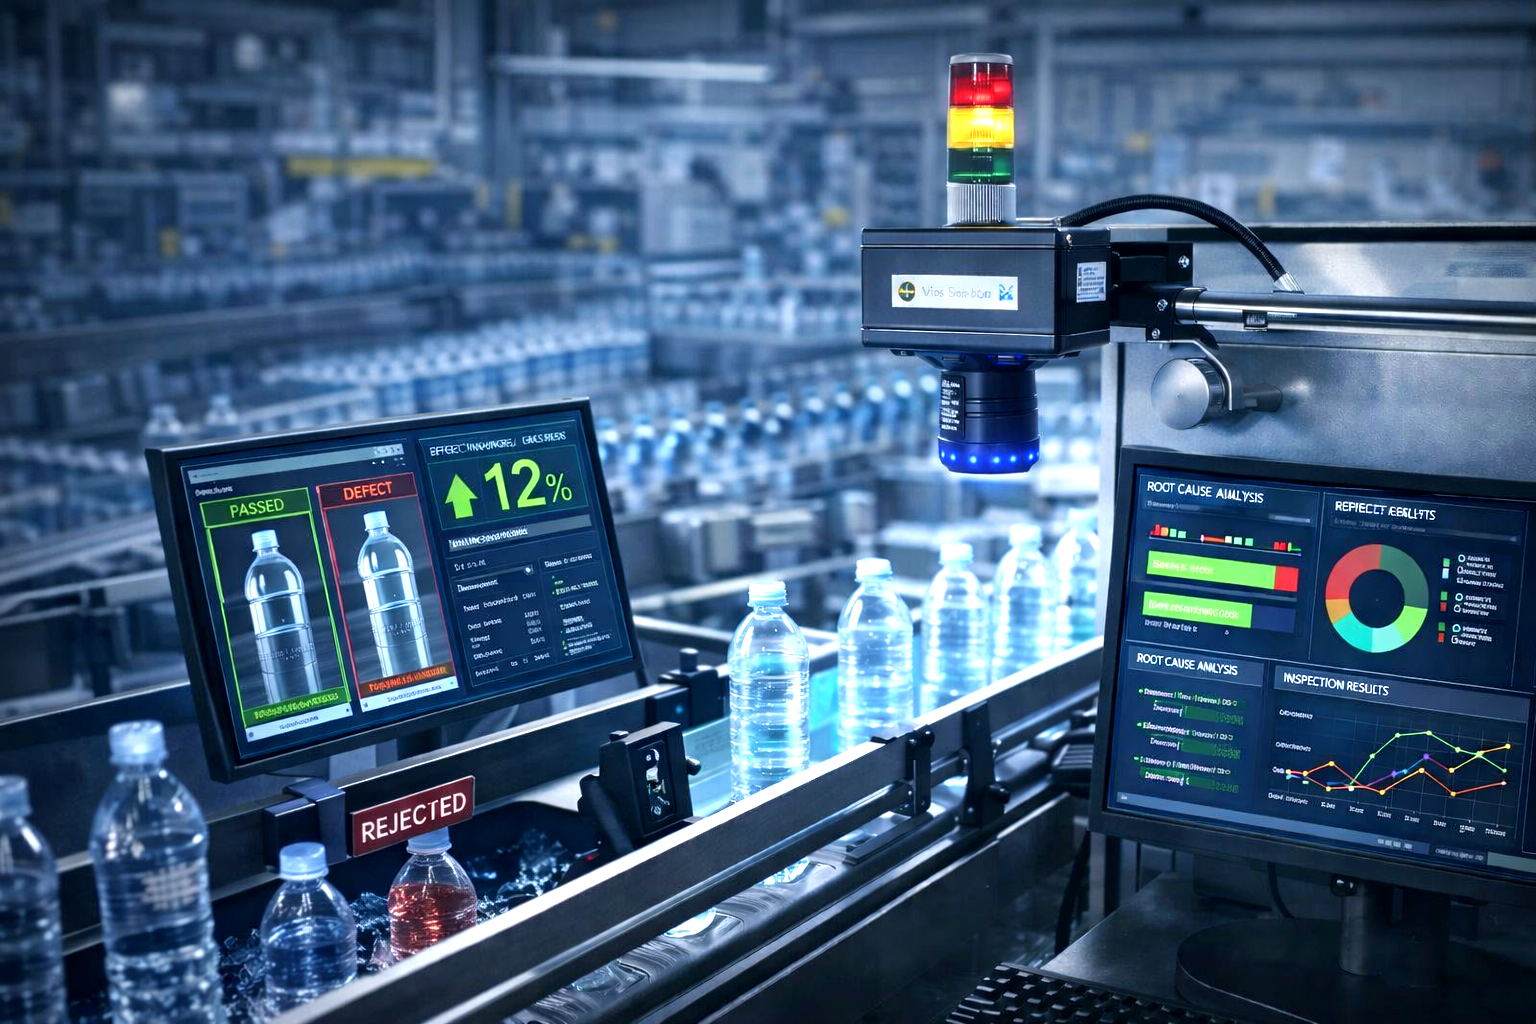
Minimize Waste, Maximize Savings
Implementing accurate inline inspection reduces the risk of defects reaching the market, cutting costs tied to recalls and rework. Early issue detection and data-driven root cause analysis help streamline operations, reduce material waste and lower overall QC expenditure.
Read MoreComputer Vision Passion
Success Stories
R&D Manager - Textile Industry
Processing Engineer - Food
Operations Manager - Electronic
We will be happy to answer you
© Copyright 2025. TR2 srls All Rights Reserved